English
 Português
 Español
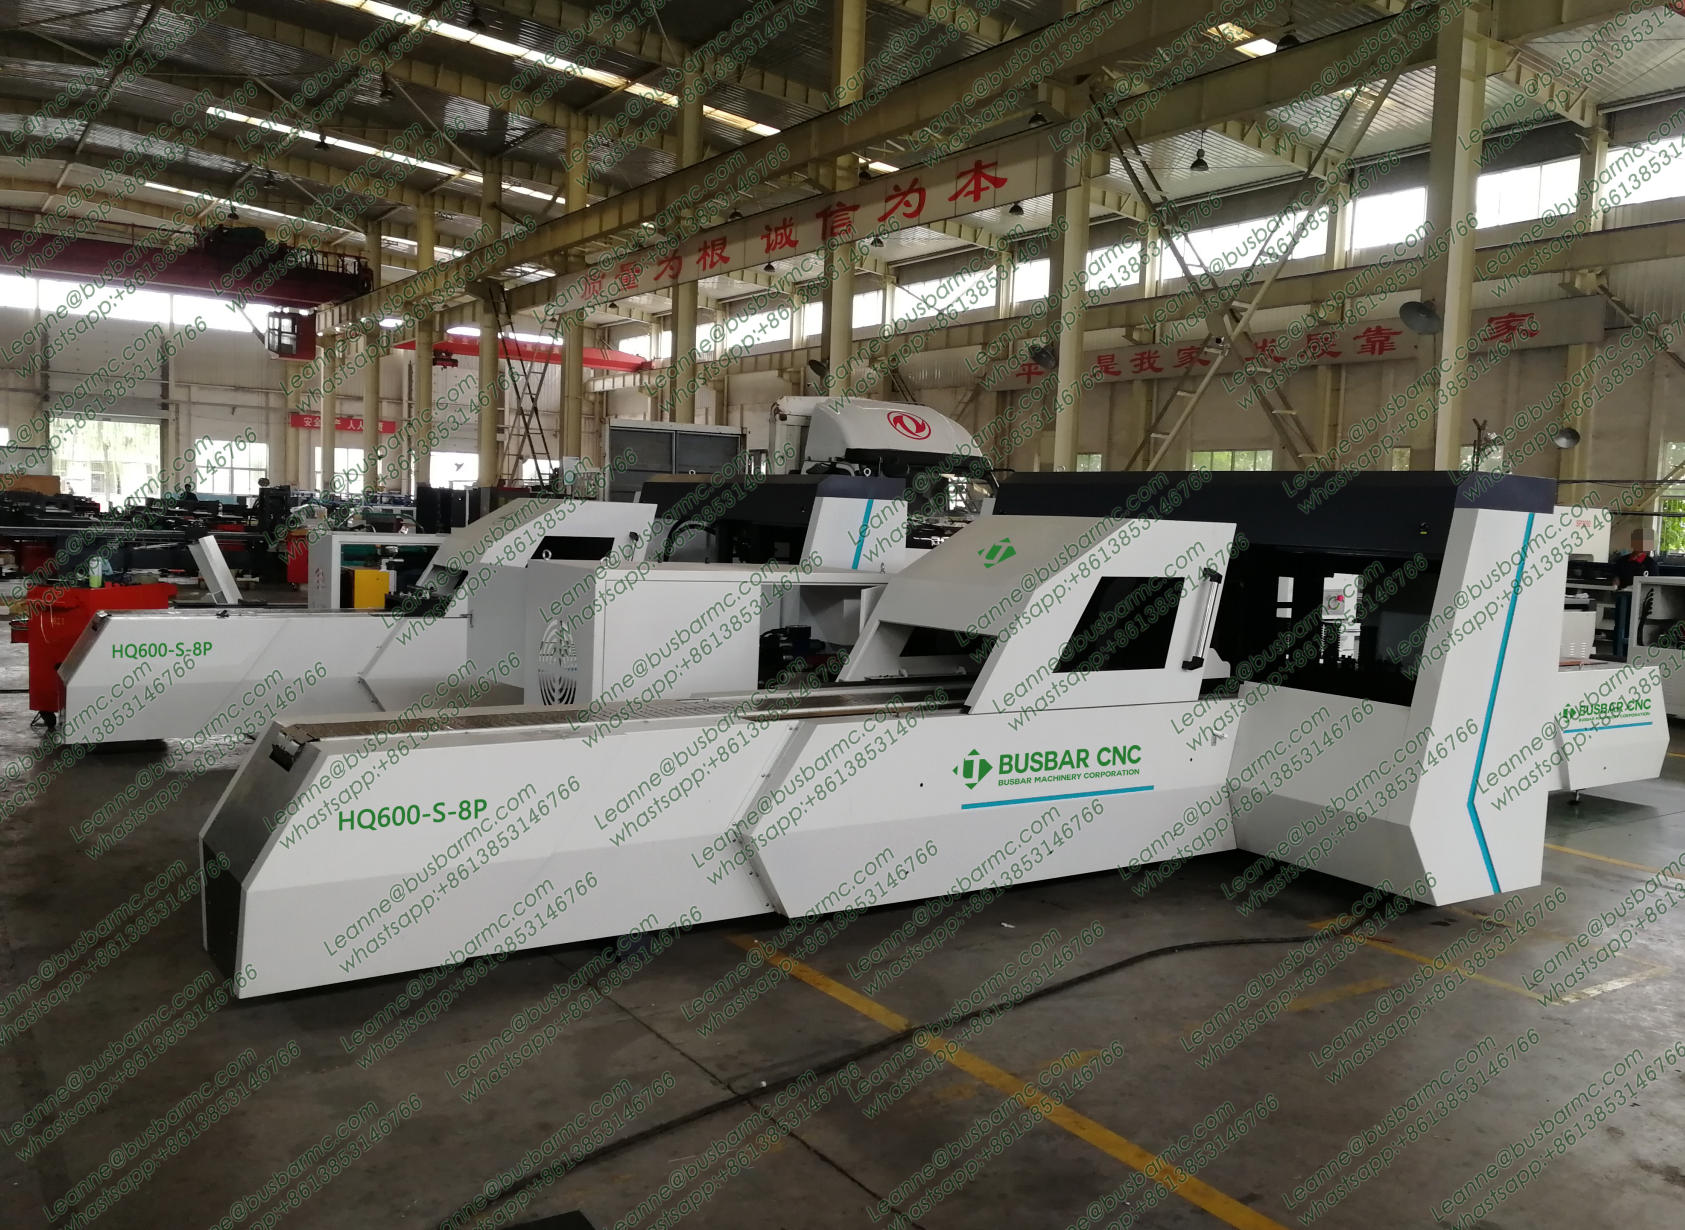
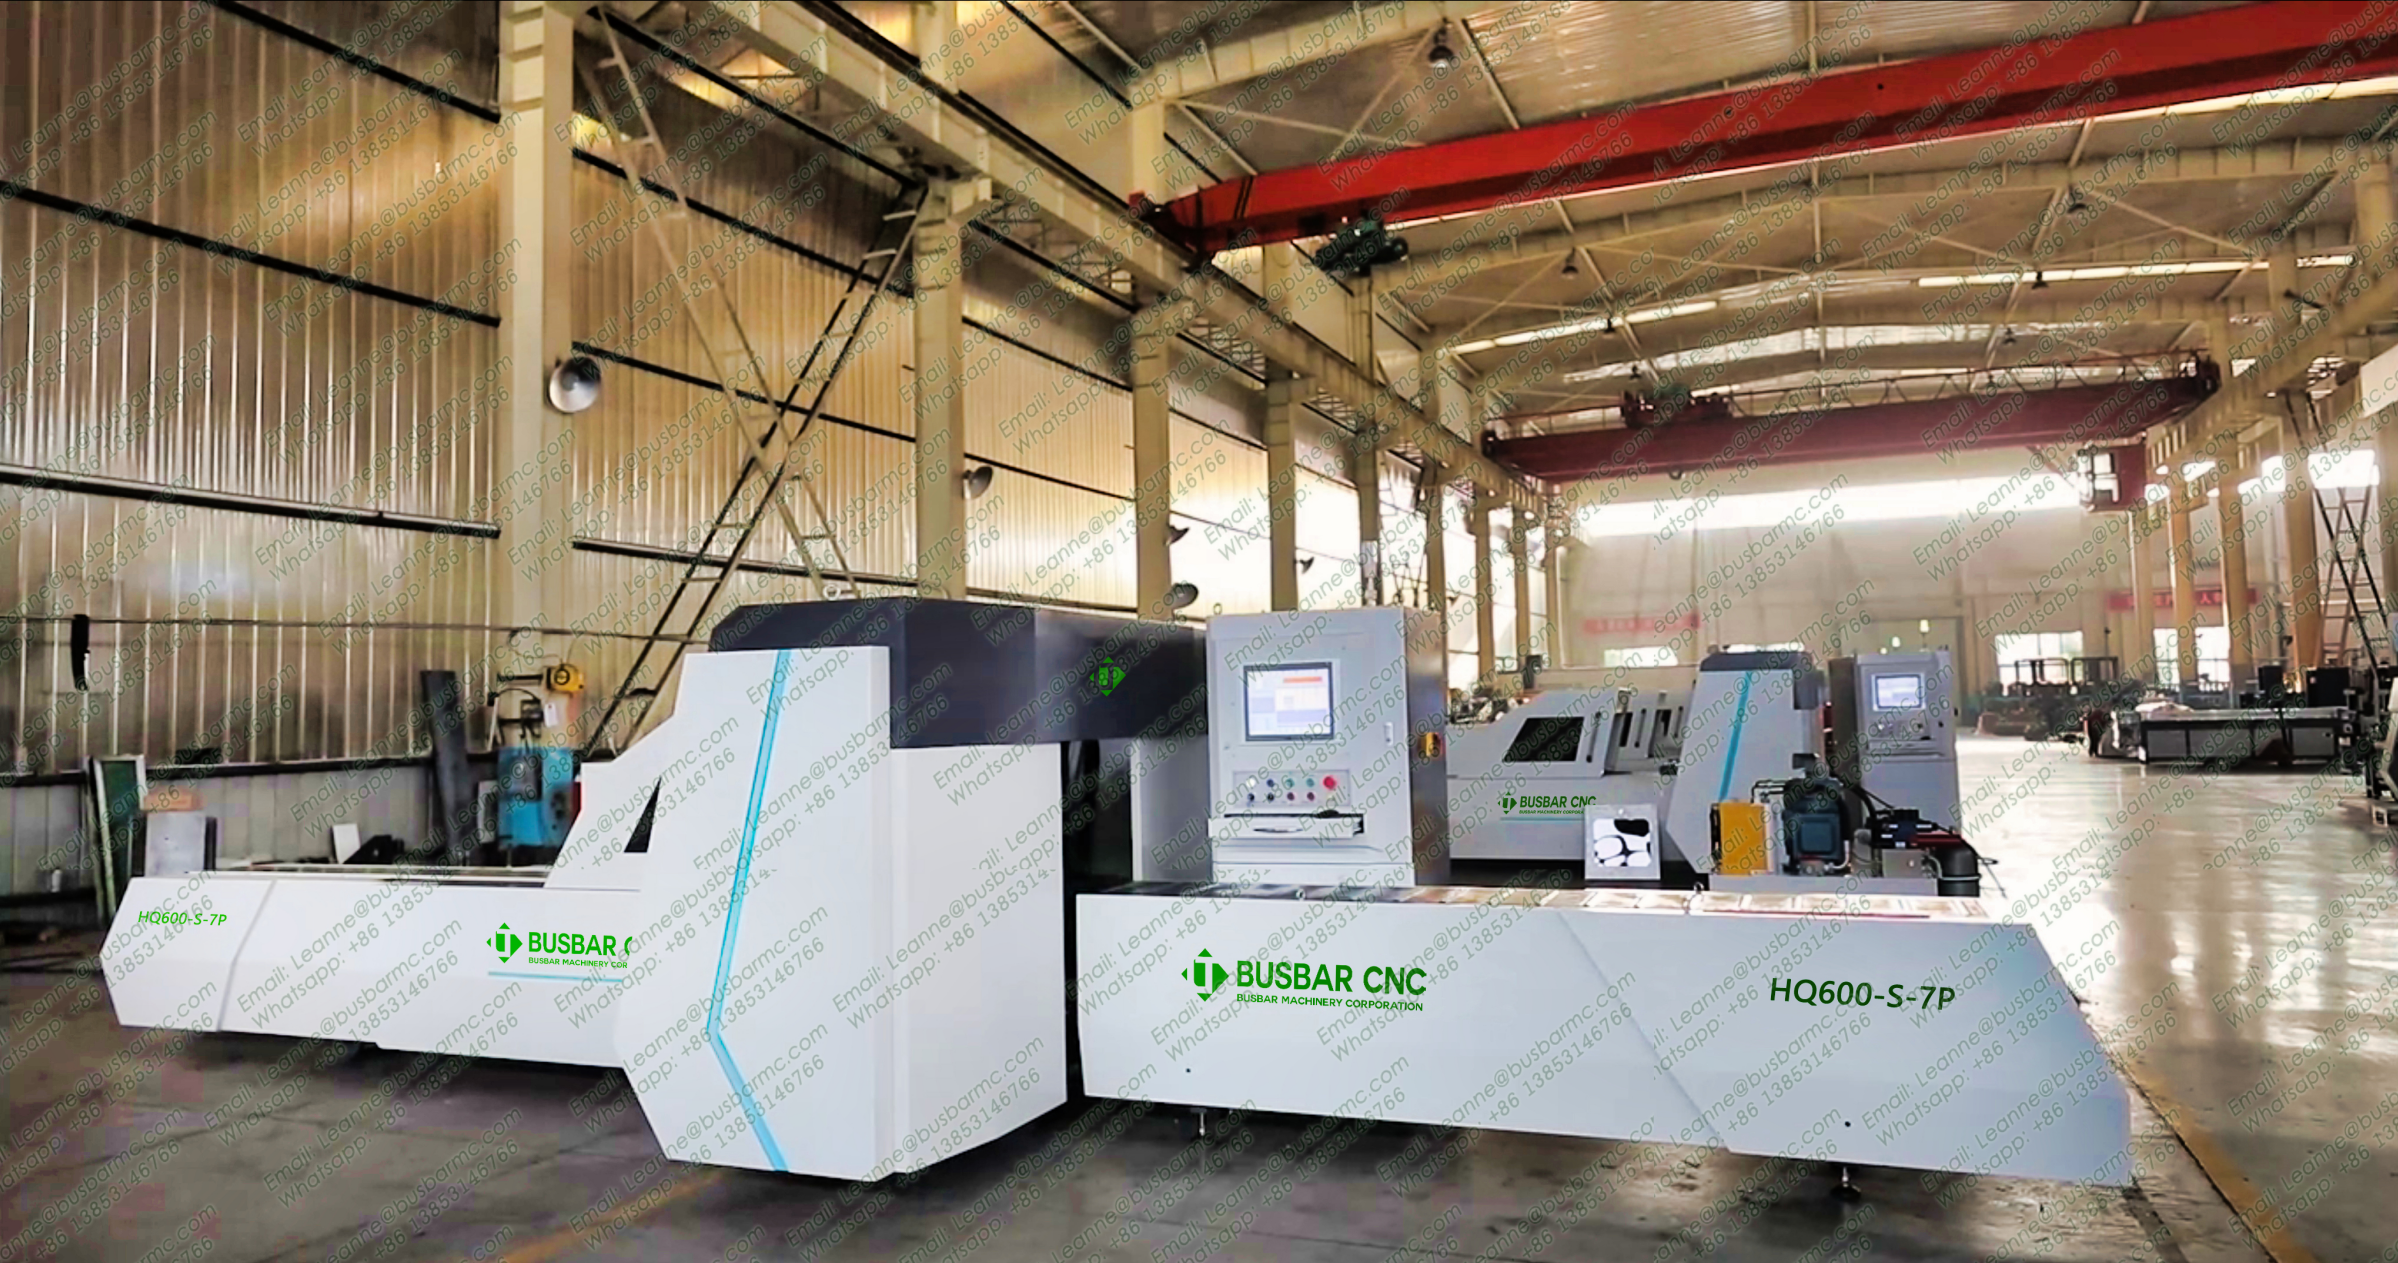
Quick answer: in LV/MV switchboard production, the bender is used after cutting and punching, with the drawing in view, the correct radius die and a material-specific springback table. The operator positions the bar, selects HMI mode (automatic or manual) and releases a first article that is measured before the batch is launched. On the LT 303U-3-C, 503U-3-C and 803U-3-C 3-in-1 machines, that station shares the frame with cut and punch.
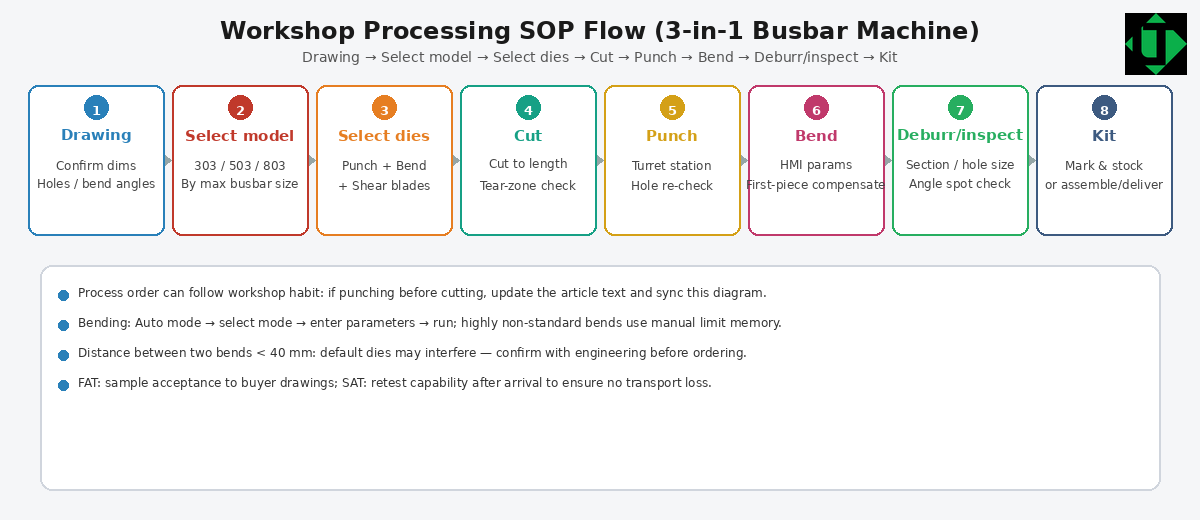
Workshop working sequence
- Read the drawing: material, temper, radius, angle, leg length and whether the bend is flat or edge.
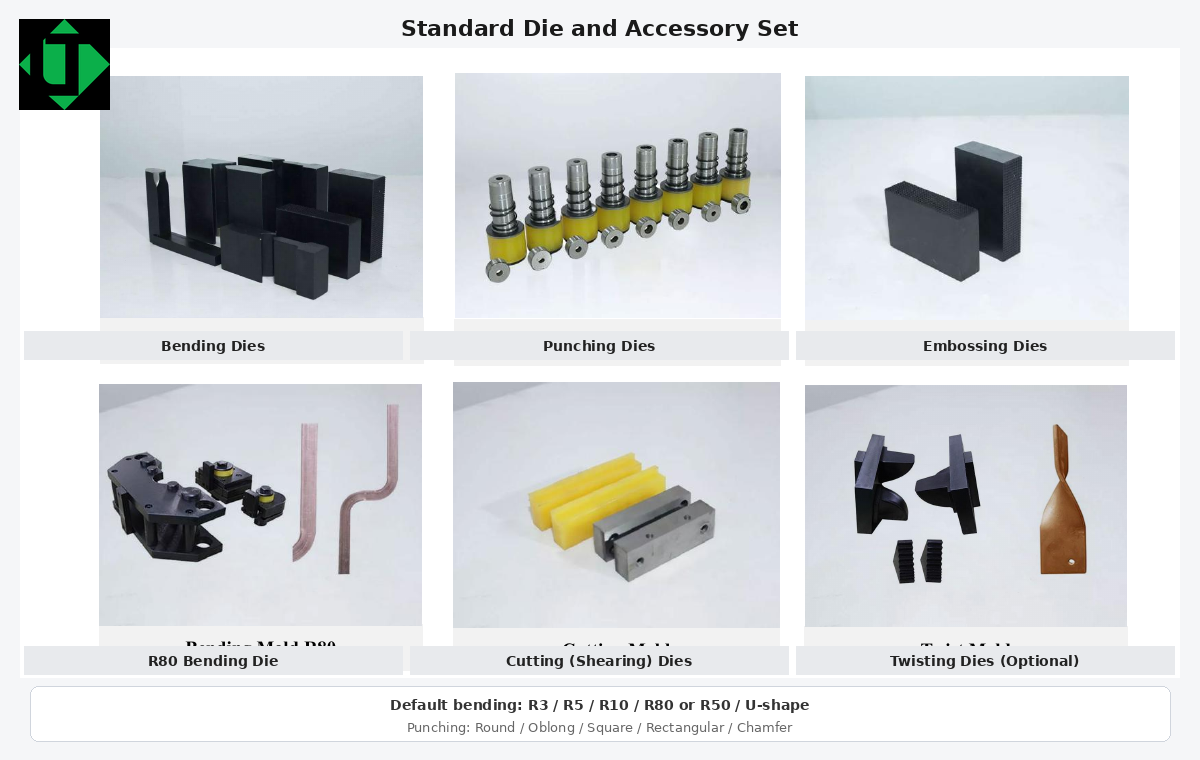
- Select the die (R3, R5, R10, R80 or R50, or a U-die) and check that it is not worn.
- Load or confirm the copper or aluminum springback table; do not mix programs.
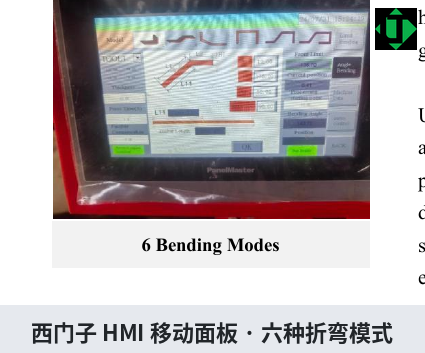
- On the HMI, use automatic mode (length, thickness, angle) or set stroke limits in manual mode.
- Make a first article, measure angle, radius and dimensions, and only then launch the run.
- Inspect burrs or die marks that could block assembly of an IRAM/IEC switchboard.
Practices that avoid rework on LV/MV switchboards
- Do not paste a copper program onto aluminum without a trial.
- Have engineering review bends with spacing under about 40 mm.
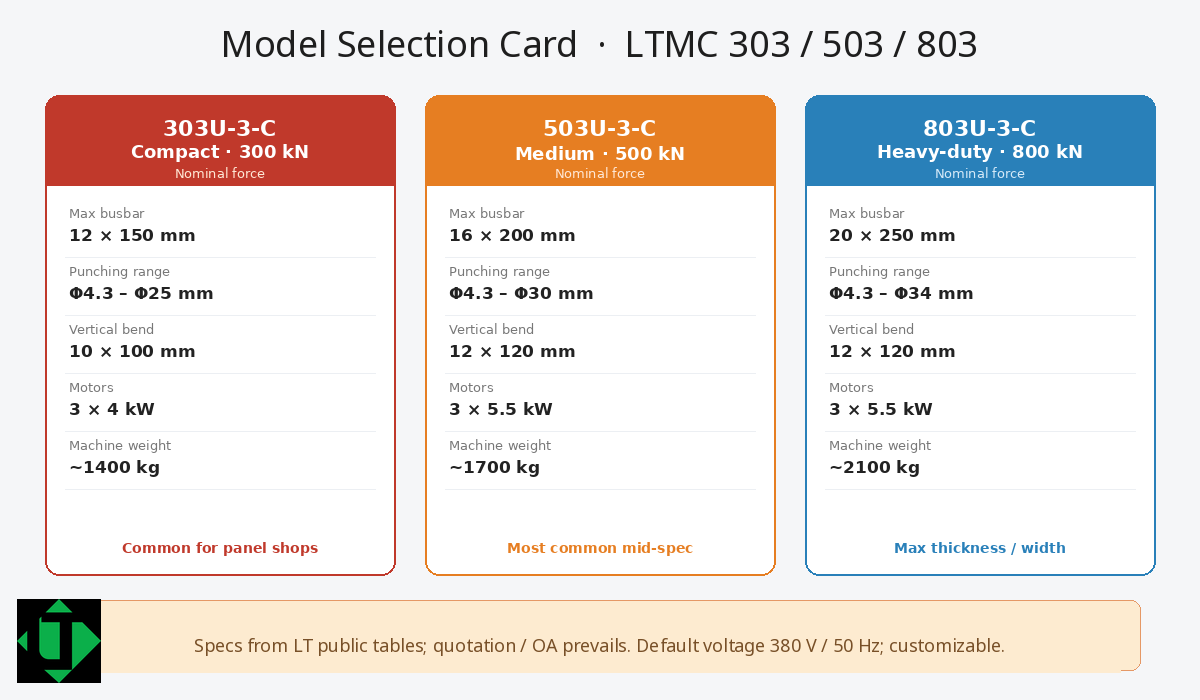
- Respect the vertical-bend envelope: 10×100 mm on 303 and 12×120 mm on 503 and 803.
- In a Buenos Aires, Córdoba or Rosario shop, kit bars by switchboard so dimensions from different drawings are not mixed.
Run control and FAT
For FAT or a production run, measure first, middle and last parts with the same instrument. Published angle tolerance is ±1° / ±0.5°, to be verified on the offer. A single showpiece does not represent the batch that is assembled in the switchboard.
Frequently asked questions
In what order is work done on a 3-in-1?
The usual order is cut, punch and then bend, so that a misplaced bend does not shift holes already made. Confirm the order on the shop drawing.
When is HMI manual mode used?
On unconventional bends or when stroke limits are set. Automatic mode covers the usual length, thickness and angle combination.
What is measured on each bar in the run?
At least the released angle and leg dimensions and, on a sample, the radius and surface. The shop sets the frequency; FAT should write it down.
How to request a quotation
For a quotation, send drawings, material (copper or aluminum and temper), maximum width × thickness, the hole and bend list, tolerances and supply voltage to [email protected] or WhatsApp +86 13853146766. More information: https://www.busductmachine.com/.