English
 Português
 Español
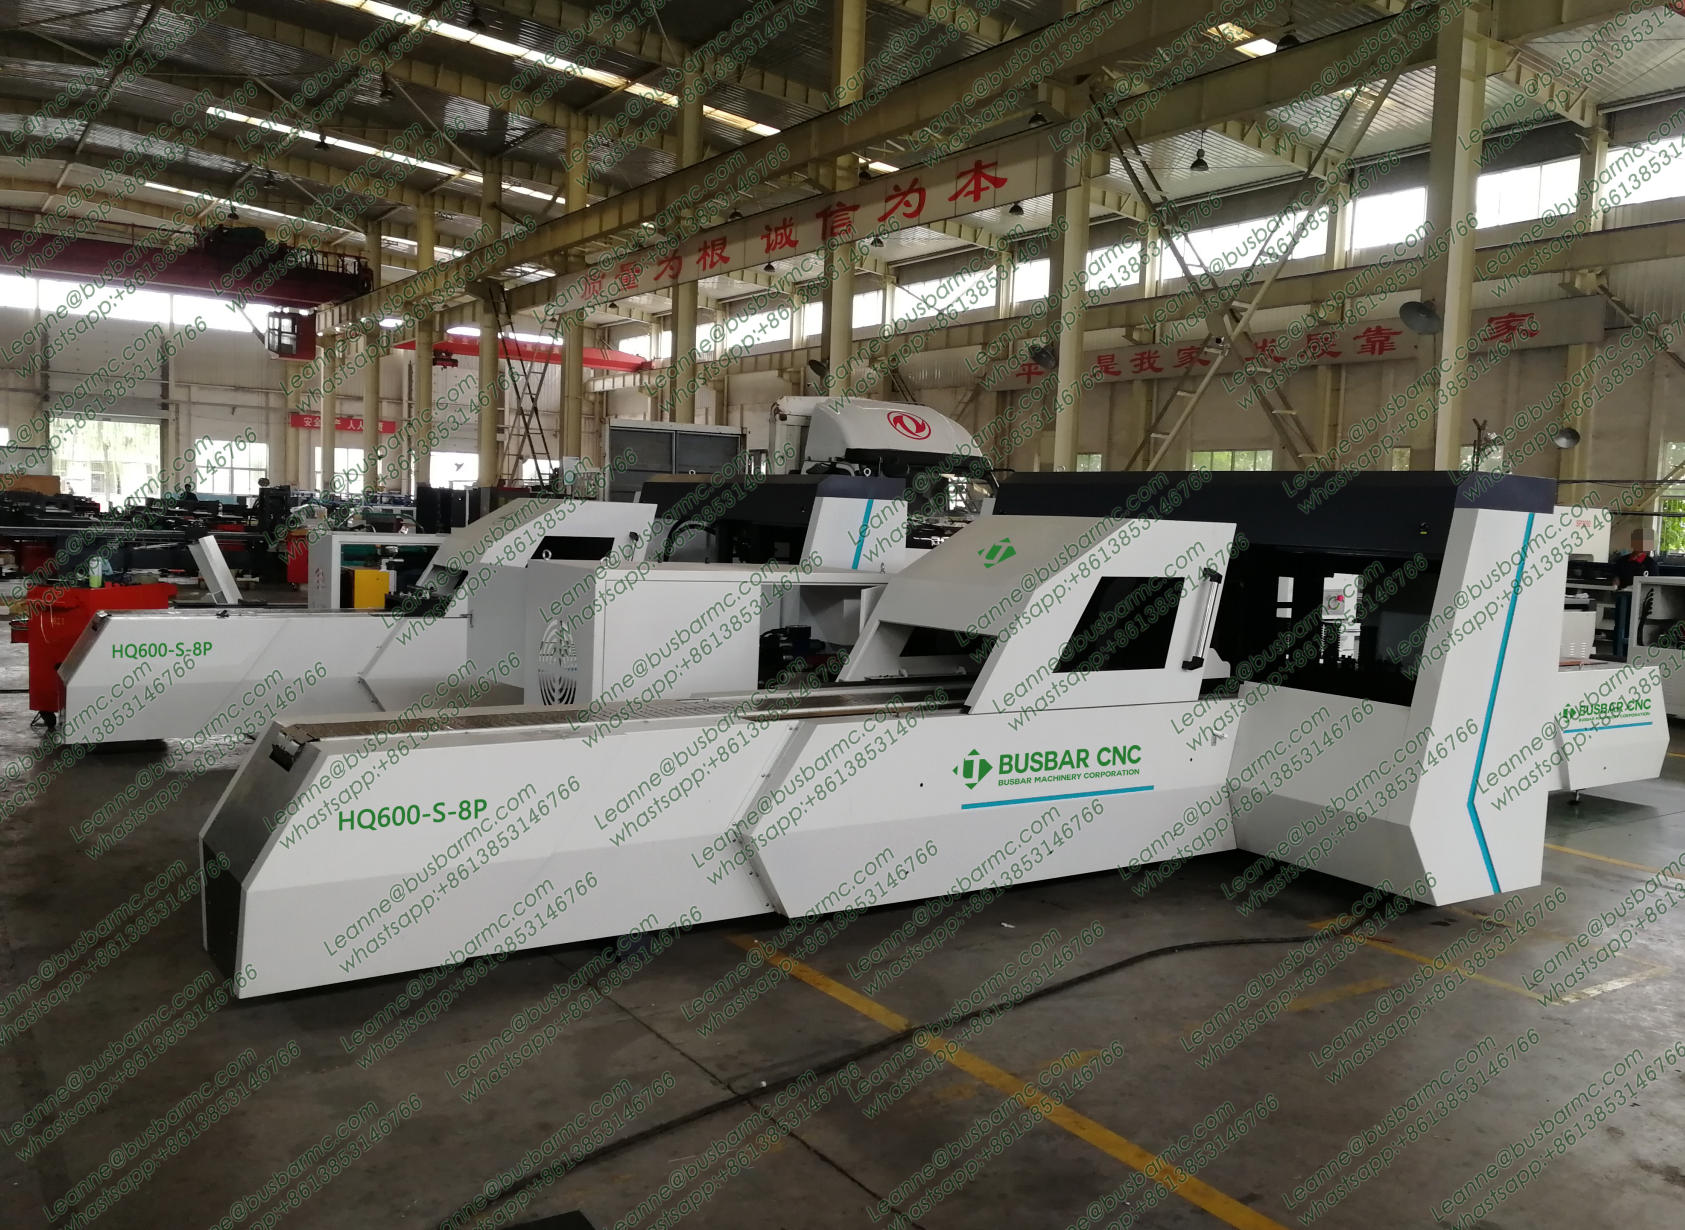
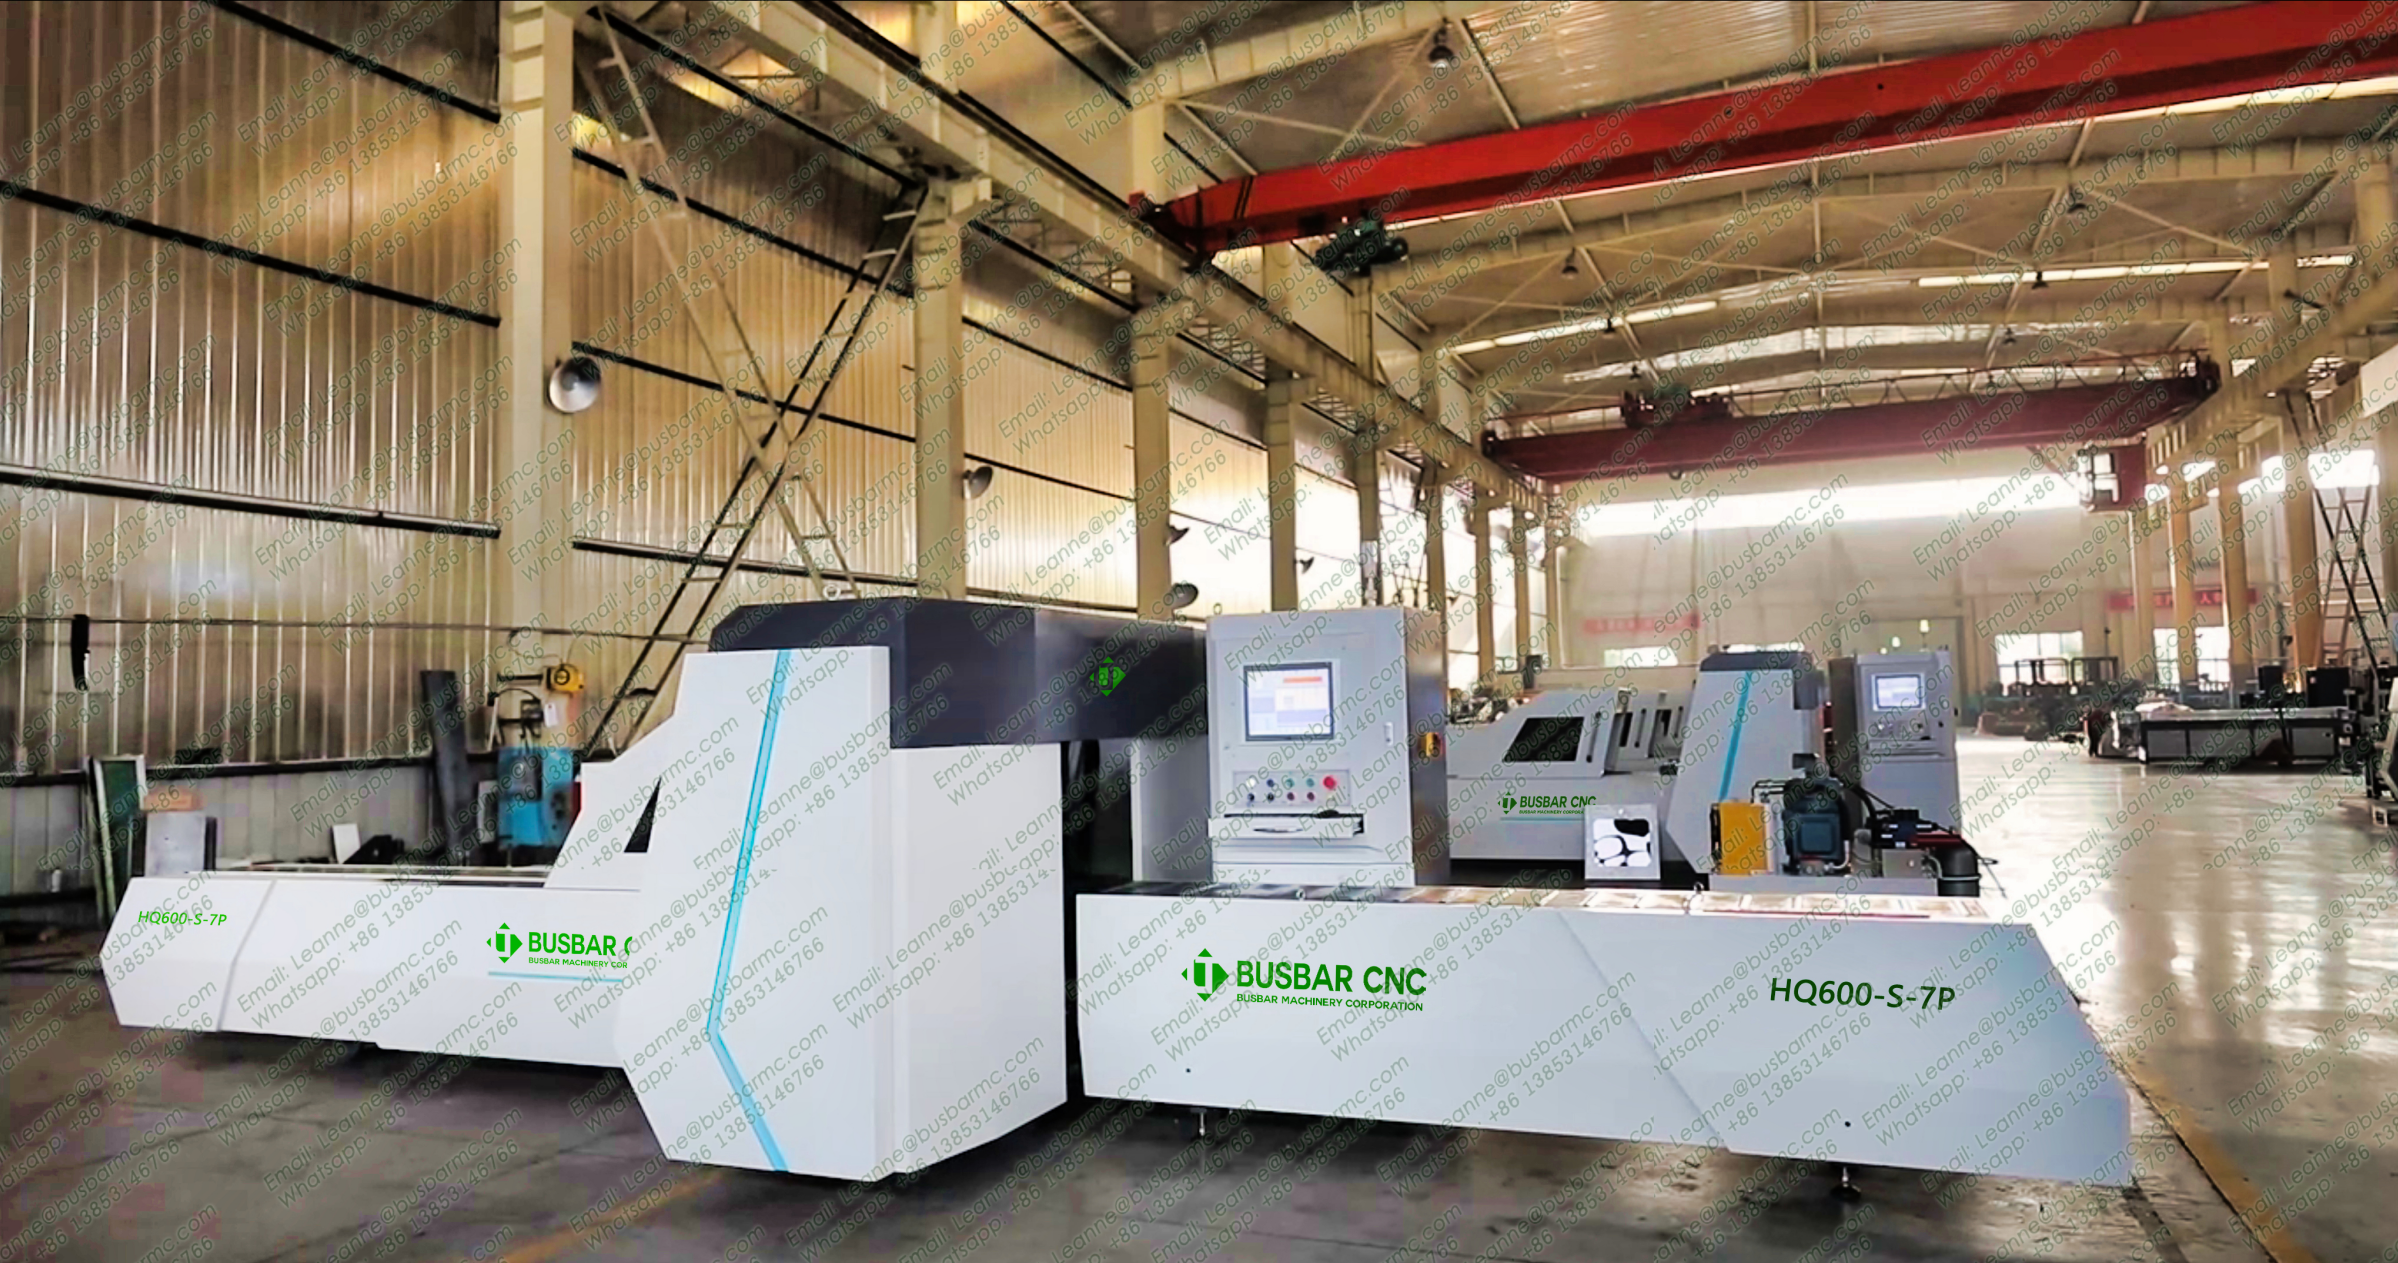
Quick answer: a busbar machine with CNC assistance or HMI recipes — such as the LT 303U-3-C, 503U-3-C and 803U-3-C 3-in-1 models — speeds up a switchboard shop when it cuts rework, shortens time to the first good part and lets a drawing be repeated without resetting from memory. Efficiency is not just stroke time: it includes die change, handling, measurement and the batch that actually ships conforming for an IRAM/IEC switchboard.
What efficiency means in a switchboard shop
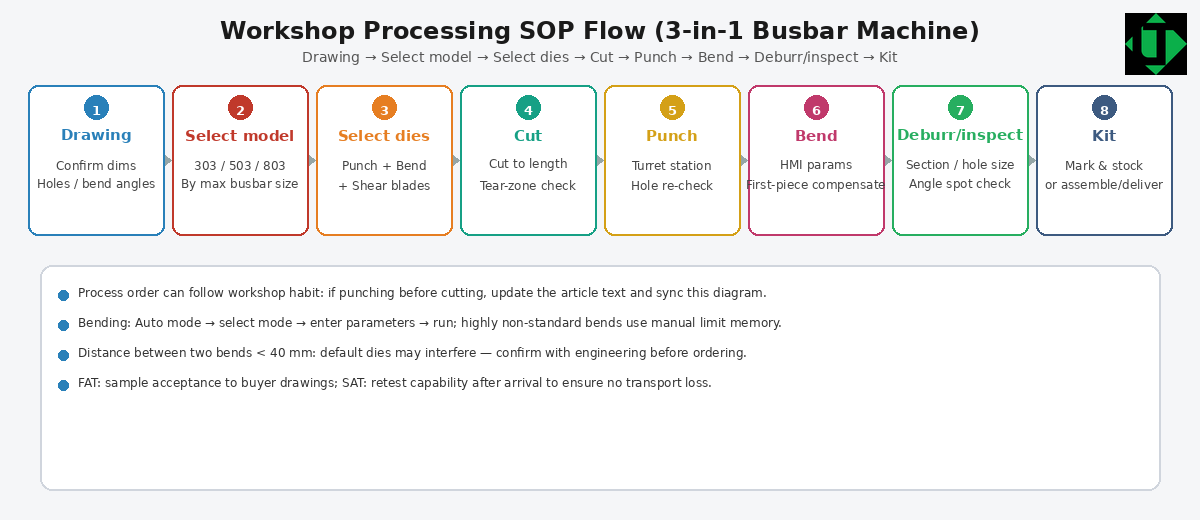
In Buenos Aires, Córdoba or Rosario, the bottleneck is rarely the press alone. A busbar kit for an LV/MV switchboard mixes different cuts, holes and bends. If every bar is measured by hand and corrected after assembly, time goes into rework. CNC or the HMI helps when it stores lengths, angles and springback compensations, and when the operator can return to a proven drawing.
Where time is really saved
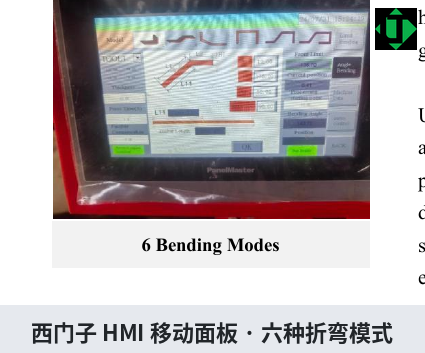
- First article: the HMI automatic mode (length, thickness, angle) cuts trial-and-error.
- Repeat drawings: a switchboard built several times for the same customer or for Mercosur export keeps its springback table.
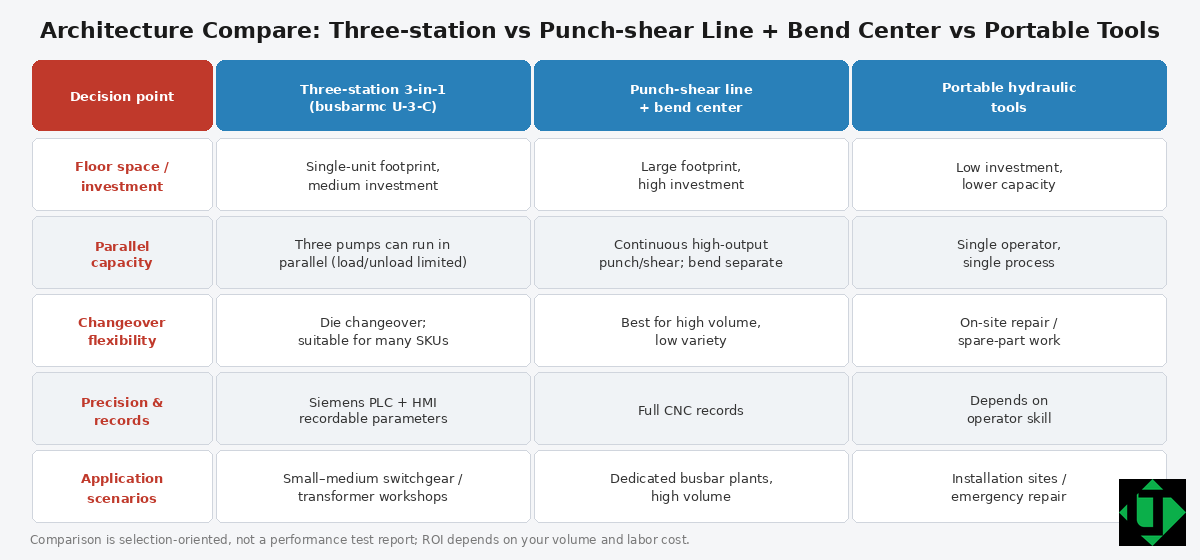
- Parallel work: on a U-3-C with three pump groups, punch, cut and bend can advance together when staffing and safety allow.
- Less rework at switchboard assembly: a hole or angle off tolerance is paid for on the floor, not in the brochure.
What CNC does not do by itself
CNC does not make bar feeding fully automatic unless that is specified. The operator still places and guides the flat at each station. It also does not replace a worn die or a wrong clearance. Efficiency is sustained with sound tooling, a copper springback table separate from aluminum, and FAT with instruments.
How to measure the improvement at FAT and on the floor
Agree a short run of the same drawing, with first, middle and last parts. Record complete cycle time, rework and length or angle deviations. Without that baseline, an efficiency claim cannot be compared across a hydraulic 3-in-1, a recipe-assisted unit and a dedicated line.
Frequently asked questions
Does a CNC busbar machine eliminate rework?
Not by itself. It reduces rework when recipes, dies and FAT are aligned with the switchboard drawing.
Does CNC feed the bar automatically?
On LT 3-in-1 machines in this series, the operator places and positions the bar at each station. The HMI helps with measurement; it does not mean automatic feeding unless specified.
How do I choose 303, 503 or 803 for efficiency?
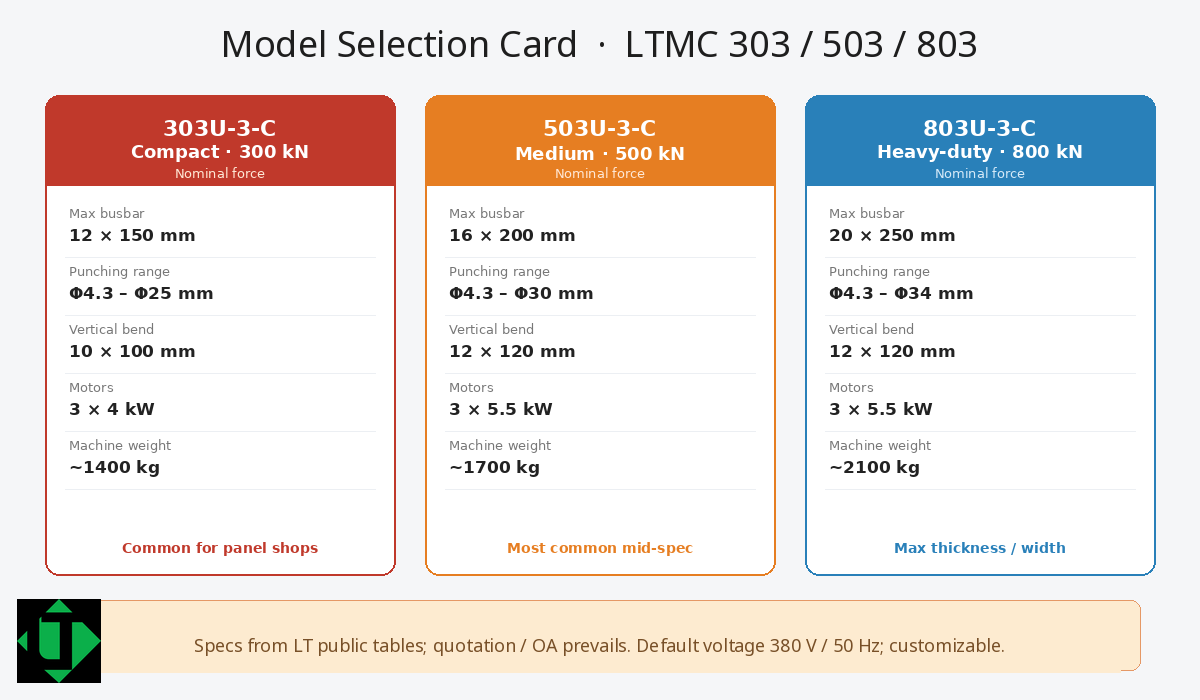
By the hardest width × thickness and hole or bend job. An undersized machine forces manual exceptions that eat the time saving.
How to request a quotation
For a quotation, send drawings, material (copper or aluminum and temper), maximum width × thickness, the hole and bend list, tolerances and supply voltage to [email protected] or WhatsApp +86 13853146766. More information: https://www.busductmachine.com/.